Why Testing is Crucial for Project Health? A project can look almost complete long before anyone can confidently say it is ready. The equipment is installed. The drawings have been updated. The punch list is getting shorter. Reports show progress, and everyone is preparing for the next milestone. Then someone asks a simple question:
Does the delivered system actually work as intended?
That question changes the character of the project.
During execution, we spend enormous effort controlling scope, resolving interfaces, following progress, managing changes, and watching for the early warnings that can push a project away from its intended path. But eventually, the project has to face reality. The system must be tested, operated, and challenged under conditions that increasingly resemble the environment where the customer will depend on it.
This is where testing becomes much more than a collection of checklists and acceptance signatures.
A Factory Acceptance Test may demonstrate that equipment or a package performs against defined conditions before shipment. Installation verification can confirm that what arrived was actually installed as intended. Pre-commissioning establishes readiness. Commissioning brings systems together. Site Acceptance Testing examines performance in the real site environment. Performance testing then asks whether the agreed results have actually been achieved.
Each step answers a different question. And that distinction matters because “it works” is not necessarily the same as “it works for the client.”
We have already discussed how inherited OEM assumptions can satisfy contractual requirements while still leaving gaps between engineering intent and operational reality. We have also explored how project teams can detect warnings before those gaps become expensive or difficult to correct.
Now we move to the point where those earlier efforts have to prove themselves. Testing is where engineering intent meets physical reality, where interfaces are challenged, where assumptions are exposed, and where the project begins to demonstrate whether the delivered solution can genuinely support the operation it was built for.
The objective is not simply to pass a test. The objective is to build confidence that the system is ready for the reality that comes next.

FAT — The First Proof, Not the Final Answer
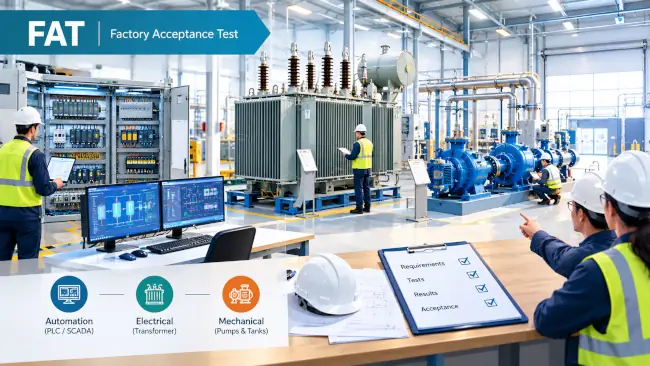
Project testing starts long before the equipment reaches the customer’s site. The Factory Acceptance Test (FAT) gives the project team an early opportunity to verify what the supplier has built. It brings the approved requirements, drawings, specifications, and functional expectations together in a controlled environment.
A good FAT should provide more than a completed checklist and a signed acceptance document. It should give the customer and supplier clear evidence that the equipment performs according to the agreed requirements. It should also create an opportunity to identify questions, clarify interfaces, and resolve findings before transportation and installation.
The testing approach naturally changes with the type of equipment. An automation system requires functional testing of PLC logic, SCADA operation, alarms, sequences, and interfaces. A transformer requires electrical tests, protection checks, and verification of its associated systems. Mechanical equipment requires attention to construction quality, dimensions, materials, and functional performance.
This makes FAT an important project milestone, but it remains only the first layer of proof. Factory conditions provide a controlled environment, while the customer will eventually operate the equipment within a much more complex site environment.
The real value of FAT therefore comes from understanding what has been built, what remains to be proven, and what the project team must carry forward to site.
That distinction becomes important throughout the testing journey. Passing FAT gives the project confidence to move a step forward, while the next stages will confirm whether that confidence survives installation and real operating conditions.
Automation Systems — Testing the PLC and SCADA
For an automation system, FAT should demonstrate how the control system behaves against the approved functional requirements. The team can test PLC logic, operating sequences, permissives, interlocks, alarms, trips, and shutdown functions using simulated field conditions.
SCADA testing should follow the same functional path. Engineers can verify process graphics, equipment status, commands, alarms, trends, setpoints, and operator controls. Communication between PLCs, remote I/O, drives, and other control systems can also be tested before the system reaches site.
A useful FAT does not simply check whether each signal appears on a screen. It follows the complete chain from the simulated field condition to the PLC response and the corresponding SCADA indication. For example, a simulated pump failure should produce the expected PLC response, alarm, equipment status, and operator indication.
The team can also challenge abnormal conditions. They can confirm that an interlock prevents an unsafe sequence or that a defined trip produces the expected response. These tests give the customer greater confidence in the control philosophy before installation begins.
FAT also provides an excellent opportunity for operators and maintenance personnel to become familiar with the system. They can review the control sequences, alarm behaviour, equipment status, and troubleshooting information while the supplier’s specialists remain available.
Electrical Systems — Testing Transformers and Protection
Electrical FAT focuses on proving the equipment’s specified characteristics and confirming the associated protection and monitoring functions. For a transformer, the agreed test programme may include winding resistance, ratio verification, insulation-related tests, and other routine or specified tests.
The team should also review the transformer’s auxiliary systems and monitoring functions. Depending on the design, these may include temperature monitoring, cooling systems, alarms, trips, local indications, and connections to protection or control panels.
Protection functions deserve particular attention because they connect the equipment to the wider electrical system. The testing team can verify the relevant settings, signals, alarms, and trip functions against the approved protection philosophy.
Documentation forms another important part of electrical FAT. Test certificates, nameplate information, drawings, approved technical data, and inspection records should describe the same equipment that will reach the site.
For larger electrical packages, FAT can also verify interfaces with switchgear, protection systems, control systems, and communication networks. This creates a stronger starting point for site installation and commissioning.
Maintenance Coupons
Maintenance Coupons
Mechanical Systems — Testing Construction, Tanks, and Pumps
Mechanical FAT takes several forms because the equipment can range from fabricated structures to complete rotating machines. The test programme should therefore reflect the equipment’s design, service, and agreed acceptance criteria.
For tanks and mechanical constructions, inspection can cover dimensions, materials, welds, coatings, connections, supports, and other specified fabrication requirements. Dimensional checks become especially useful where the equipment connects with piping, instruments, pumps, or structures supplied by other parties.
For pumps, FAT can combine mechanical inspection with agreed performance testing. Depending on the pump and specification, the team may verify flow, pressure, speed, vibration, power consumption, and other relevant parameters.
Auxiliary systems also deserve attention. Lubrication, cooling, seals, instrumentation, local controls, and other supporting arrangements can influence the equipment’s performance during operation.
Mechanical FAT therefore creates documented evidence about both construction and performance. It also gives the project team an opportunity to identify interface requirements before the equipment reaches a site where several contractors may be working simultaneously.
From Factory Proof to Site Reality
These three examples show why FAT should follow the equipment’s actual function rather than a generic checklist. Automation, electrical, and mechanical systems require different tests, but they share the same objective: to establish reliable evidence before the equipment enters the customer’s environment.
That evidence becomes the reference point for the next stage of the testing journey.
Once the equipment reaches site, the project faces a different question:
Did we install what we tested? let’s answer it in coming posts.
If you feel you need help with any of these ideas we discussed, request a Management Consultancy or Coaching Services From our Store